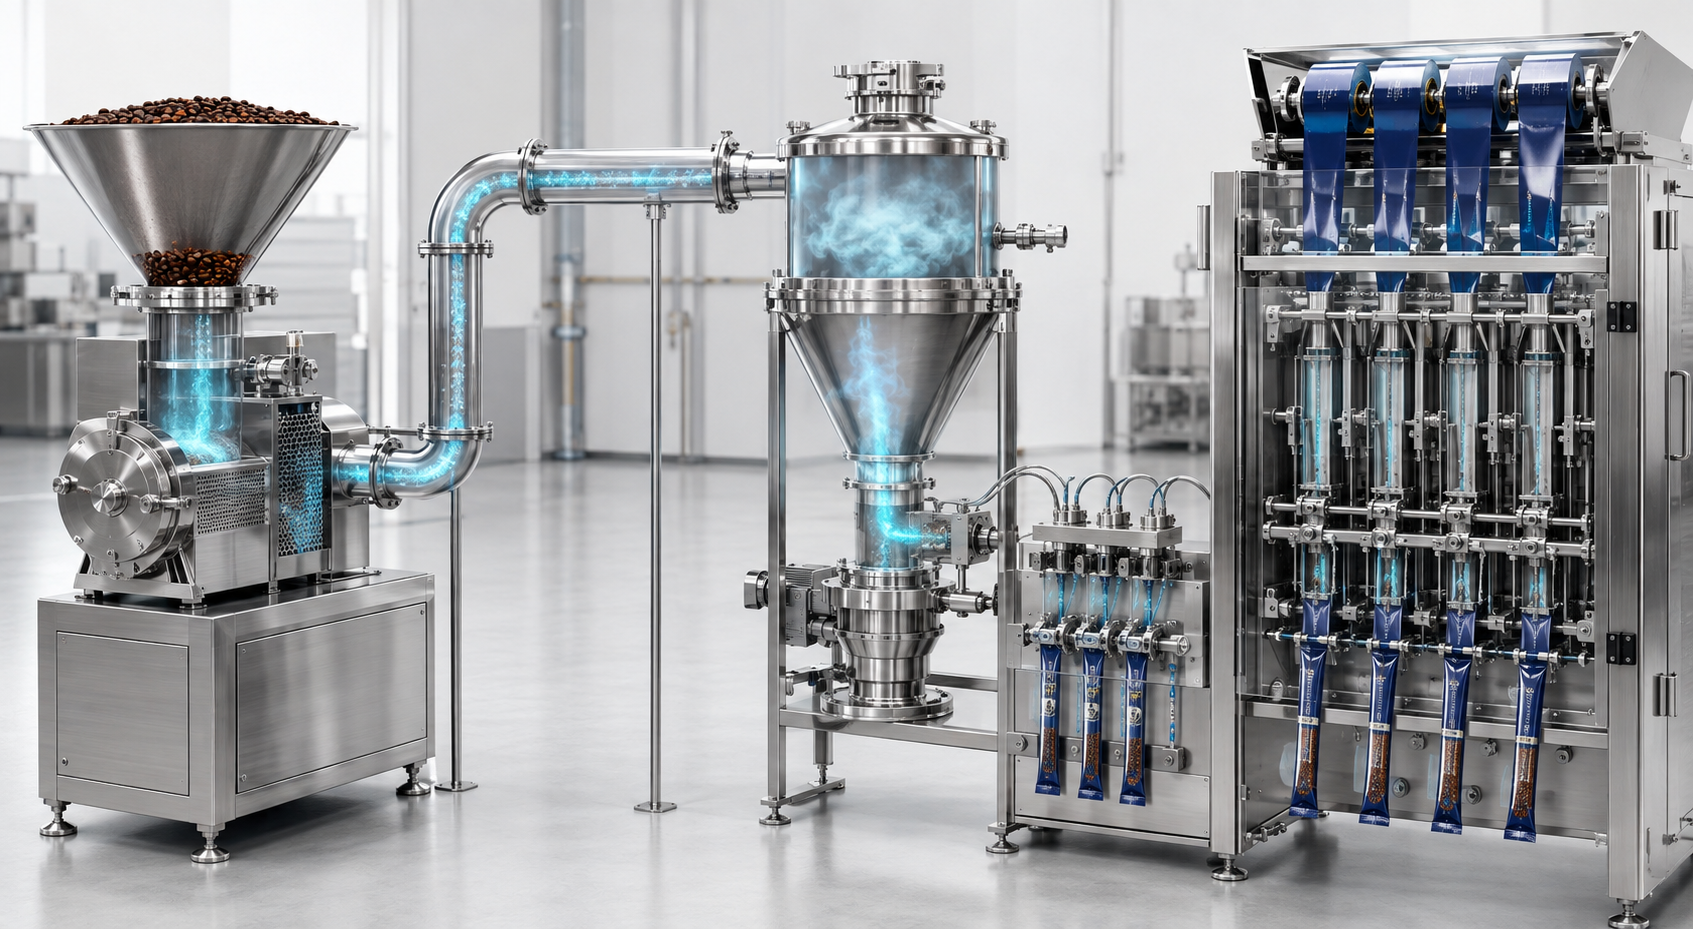
After the coffee is ground, the surface area increases rapidly, and the aroma substance is more likely to volatilize and oxidize. Therefore, the lock should not only rely on the first nitrogen filling before the sealing, but should regard the grinder outlet, buffer bin, conveying pipeline, metering hopper, Stick filling area and gas replacement in the bag as a continuous oxygen exposure control system. The system design first needs to identify the position of air intake, and reduce the oxygen inclusion of materials during the cache, feed and feeding process through closed connection, stable material level, low disturbance conveying and partitioning. For different protection areas, flow control, pressure monitoring and necessary oxygen content detection should be set up respectively, and a recursive nitrogen filling formula should be established according to product characteristics, packaging speed and bag type. Bag internal replacement must also be coordinated with the blanking, film operation and horizontal seal timing. If the air flow is too small, the air cannot be fully replaced, and if the air is too large, the coffee dust may be raised and the sealing area may be polluted. DOT combined with the Joyea Stick packaging platform, through real material and packaging material test, comprehensive verification of residual oxygen, sealing integrity, dust control, nitrogen consumption and operation stability in the bag. At the same time, it is equipped with environmental oxygen monitoring, ventilation, low-pressure alarm and safety interlocking, so that the coffee lock is fresh, the production safety and long-term stable operation to form a complete project closed loop.
C02 · PACKAGING ENGINEERING NOTE
Coffee-filled fresh-locking system from grinding to sealing: oxygen exposure control, airtight transport, bag in-place replacement and safety management engineering methods
The aroma protection of coffee should not only rely on the first nitrogen filling before the packaging bag is sealed. Oxygen may continue to enter the product during buffering, conveying, metering and blanking. DOT regards grinder outlets, confined buffer chambers, low perturbation delivery, STIC filling areas and bag gas replacement in bags as a continuous oxygen exposure control system, and is equipped with the JOYEA packaging platform to configure oxygen content monitoring, nitrogen management, dust removal and personnel safety interlocking.
Identify Where Oxygen Enters the Process
The first engineering task is to identify air-ingress points instead of simply increasing nitrogen flow. Typical entry locations include the grinder discharge, buffer-vessel breathing points, transfer interfaces, dosing-hopper refilling, and the open package before sealing. The design should shorten exposed paths, use enclosed connections, maintain stable product levels, and divide the process into manageable protection zones. This reduces repeated purging and helps prevent large oxygen fluctuations between normal production, refilling, low-speed operation, and restart conditions. Each zone can then be monitored and controlled according to its actual risk and process function.
Create Continuous but Zoned Nitrogen Protection
The grinder outlet and buffer vessel can operate under a controlled protective atmosphere, while the conveying and dosing sections focus on preventing air entrainment. Near the forming tube, nitrogen is directed toward displacing air inside the stick before sealing. Instead of feeding every location from one unregulated branch, each functional zone should have suitable flow control, pressure supervision, and, where justified, oxygen sampling. Zoned control makes abnormalities easier to locate and allows nitrogen settings to be linked to product type, machine speed, and pack geometry through managed recipes rather than operator intuition.
Synchronize Gas Displacement with Sealing
A higher nitrogen flow does not automatically produce lower package oxygen. Nozzle position, film movement, dosing timing, product displacement, and transverse-seal closure all influence the result. Excessive flow can disturb low-density material, spread coffee dust into the sealing area, or destabilize film tracking. Development trials should therefore evaluate the complete interaction between gas delivery and the packaging cycle. Flow visualization, package oxygen measurement, seal inspection, and consumption data can be used together to establish settings that balance atmosphere replacement, product control, clean seals, stable film formation, and responsible nitrogen use.
Include Personnel Safety in the Freshness Strategy
Nitrogen can create an oxygen-deficient atmosphere, while coffee dust can introduce hygiene, housekeeping, and combustible-dust risks. The engineering package should therefore address room ventilation, ambient oxygen monitoring, gas-pressure alarms, isolation logic, exhaust routing, and the applicable hazardous-area assessment. Opening, cleaning, or maintaining protected equipment must place the gas system in a defined safe state. Operating procedures and alarm responses also need to be understandable to production and maintenance teams. Product freshness cannot be engineered separately from personnel safety, cleanability, and the regulatory requirements of the installation location.
START WITH MATERIALS AND TARGETS